Logic & operator interface
PLC and HMI programming that operators trust
We write the logic that runs your process and the screens your operators watch, so the system behaves predictably and the people on the floor know exactly what it is doing.
Code written to be maintained
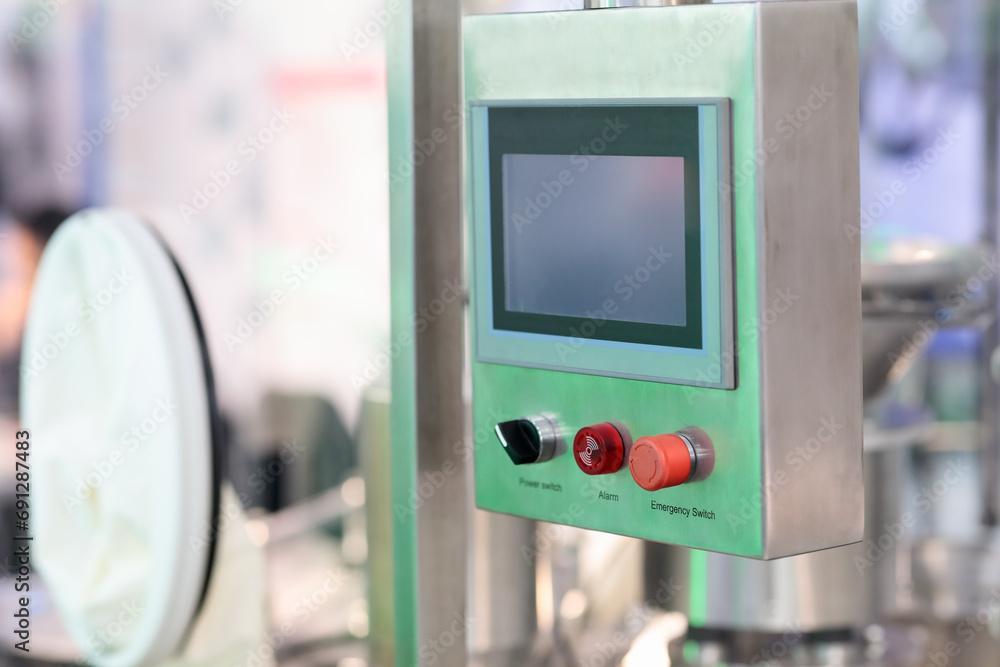
We develop PLC logic for new machines and production lines, upgrade aging controllers and rework HMI screens so operators get clear control and real-time status. Logic is structured, tags are named consistently and screens are laid out around the way your team actually runs the process, so the next technician to open the project can follow it without a phone call.
Programming happens in the same building as the panel and drive work, which means control logic, drive parameters and screen development are reconciled before the system ships, on new builds and on retrofits of existing equipment alike. Where a process needs plant-wide visibility rather than machine-level control, the same team writes the SCADA and process control layer.
What we program
Logic and interface work that ships with the panel or arrives as an upgrade.
- PLC logic
- Control programs for machines, conveyors and full lines, structured and commented so they stay maintainable.
- PLC upgrades
- Migration of older controllers to current platforms, keeping the process intact while the hardware moves forward.
- HMI screen development
- Operator screens that show status, alarms and control in a layout matched to how the line runs.
- Recipe management
- Recipe handling so operators switch products or batches without reprogramming the controller.
- Retrofit programming
- New logic and screens dropped into existing equipment, with wiring and I/O reconciled against as-built drawings.
- Documented handoff
- Control programs, HMI configurations and drive settings delivered in print and digital formats.
Need logic written or an old PLC moved forward?
Tell us the controller, the process and what the operators need to see. We will take it from there.